A casting can pass inspection and still not be stable. That usually shows up later, not at dispatch. A hole position shifts slightly across batches, a flange face needs more machining than usual, or a section behaves differently under load even though composition is correct. None of these point to a single failure. They point to drift in the process.
That is the context in which investment casting India are evaluated today. Not by whether a part can be made correctly once, but whether it can be made the same way repeatedly without pushing correction to the machining stage. Microstructure and dimensional precision are outcomes, but both are controlled much earlier, long before metal is poured.
Shell Behavior Is a Thermal Variable, Not Just a Mold
The ceramic shell is often treated like a passive form, but it controls how heat leaves the metal. That makes it part of the solidification system. If shell thickness varies across the cluster, cooling rate varies with it. Even a difference of 0.5 to 1 mm changes how fast sections lose heat, especially in walls below 4 mm.
Typical shell thickness in investment castings India sits somewhere between 7 mm and 10 mm, built over multiple slurry and stucco cycles. If slurry viscosity changes during the shift, the primary coat thickness shifts. That affects surface finish first, but it also changes how the outer shell behaves thermally.
Permeability also matters. A dense shell traps heat longer. A more open shell allows faster heat loss but can introduce surface instability if not controlled. These are not theoretical concerns. They show up as grain variation between similar parts in the same batch.
Wax Pattern Is Where Dimensional Error Starts
Dimensional deviation does not begin in metal. It starts in wax. Wax shrinkage sits roughly in the 0.4% to 0.6% range depending on composition and temperature control. If injection temperature fluctuates even by 2–3°C, shrinkage becomes uneven across the pattern.
In stable investment castings India operations, wax injection is not adjusted frequently. It is held steady. Die temperature is controlled to avoid local cooling differences. If one side of the die cools faster, the pattern pulls unevenly, and that distortion carries forward.
Once the shell is built, geometry is locked. Metal only replicates what exists. No stage after that corrects shape without adding cost.
Pouring Temperature Is Not About Maximum Fluidity
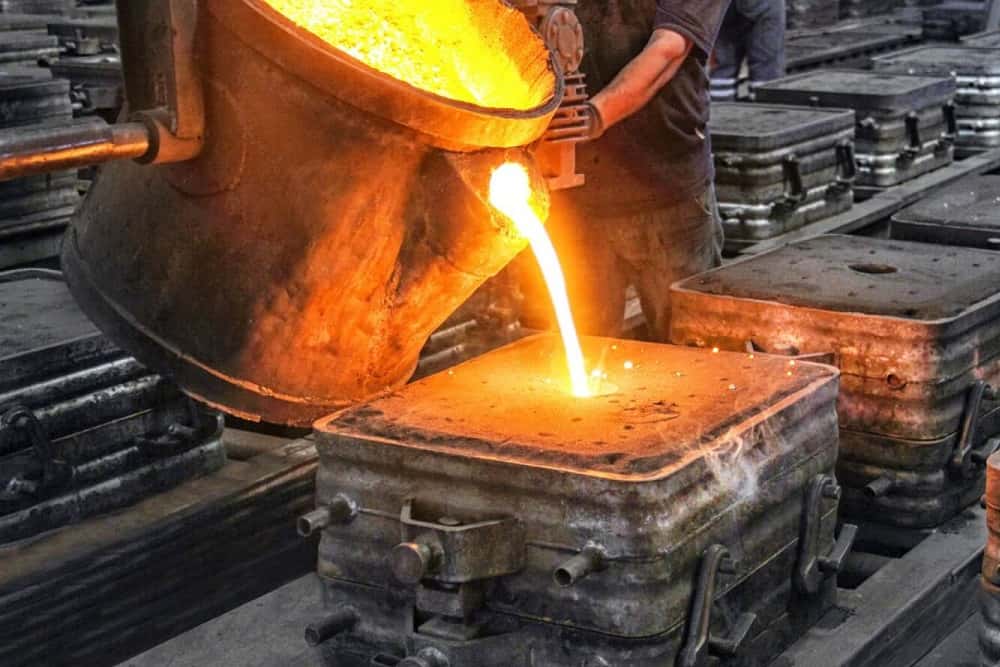
There is a tendency to run higher pouring temperatures to ensure fill, especially for complex geometries. That works for fill, but it works against structure. Higher superheat increases grain size and promotes segregation.
For stainless alloys, pouring often falls between 1560°C and 1620°C in investment castings India, but the exact point is adjusted based on section thickness. Thin sections need flow, but thicker ones do not benefit from excess temperature.
If temperature is pushed higher than required, dendrite spacing increases. That weakens mechanical consistency across the part. The issue does not appear immediately. It shows under load or fatigue.
Solidification Is Where Structure Gets Fixed
Once pouring is done, control shifts to cooling. This is where microstructure is actually set. Faster cooling leads to finer grains. Slower cooling allows coarser grains and segregation.
Directional solidification is used in better-controlled setups. The idea is simple. Metal should freeze progressively, not randomly. If solidification starts at multiple points, shrinkage pockets form in the center.
In investment castings India, this is handled through mold temperature control and gating design. Feeding must support the last solidifying zones. If feeding is not balanced, shrinkage shows up internally even if the surface looks fine.
Secondary dendrite arm spacing is often used as an internal indicator. Lower values, around 30–40 microns, generally indicate better cooling control for many alloys. Higher values suggest slower or uneven solidification.
Chemistry Alone Does Not Guarantee Performance
Spectrometer readings confirm composition, but they do not confirm structure. Two melts with identical chemistry can behave differently depending on cooling.
Carbon variation of 0.02% may not seem significant, but combined with slower cooling, it increases carbide formation in certain alloys. Sulfur, even below 0.02%, affects hot tearing risk if thermal conditions are not controlled.
This is why investment castings India are not evaluated on chemistry alone. Chemistry defines potential. Process defines outcome.
Tolerance Comes from Accumulated Control, Not Final Adjustment
Dimensional tolerance is often quoted as ±0.2 mm to ±0.4 mm depending on size. That number is not achieved in one step. It is the result of multiple stages staying within limits.
Wax shrinkage, shell expansion, metal contraction, and cooling distortion all add together. If each stage drifts slightly, total deviation increases. No single stage causes the issue. The combination does.
In stable investment castings India production, the goal is to keep each stage within a narrow band so the total stack-up stays within tolerance. Machining then becomes minimal, not corrective.
Surface Finish Is a Reflection of Process Stability
Surface roughness is typically controlled in the range of Ra 3.2 to 6.3 microns. That comes from the primary coat quality and how consistently it is applied.
If slurry viscosity changes during the day, surface texture changes. If drying conditions fluctuate, micro-cracks can form in the shell. These transfer directly to the metal surface.
Controlled drying conditions, usually with humidity around 45–60%, help maintain uniformity in investment castings India. Without that, surface variation becomes visible across batches.
Where Process Drift Starts to Show in Practice
Drift does not show as failure first. It shows as small differences that accumulate.
| What Starts Changing | Likely Source | Where It Shows | What It Leads To |
| Slight dimensional spread increase | Wax injection variation | Pattern and final casting | More machining adjustment |
| Grain becoming less uniform | Pouring temperature fluctuation | Sectioned areas | Variation in strength |
| Surface becoming rougher | Slurry inconsistency | Outer surface | Extra finishing work |
| Internal shrinkage appearing | Feeding imbalance | Core regions | Reduced reliability |
| Part distortion after cooling | Uneven cooling rate | Assembly stage | Fitment issues |
None of these stop production immediately. They increase effort later.
Control Across Stages Matters More Than Individual Excellence
A single well-controlled stage does not ensure quality. If wax is stable but shell varies, result varies. If shell is stable but pouring fluctuates, result varies.
What defines better investment castings India output is alignment across stages. Each step holds steady enough that variation does not build.
An operation like Siddhalaxmi reflects this approach by keeping process consistency across pattern, shell, and metal stages instead of depending on final inspection to catch deviation.
Where Most Precision Is Actually Lost
Precision is usually lost before anyone measures it. Once the casting is produced, inspection only detects the deviation. It does not explain where it came from.
If wax pulls unevenly, geometry is already off. If shell thickness varies, cooling will vary. If pouring temperature drifts, structure changes. By the time machining begins, these effects are already built in.
That is why high-quality investment castings India are judged by how little correction is needed, not how well correction is done.
Final Perspective
Microstructure and dimensional precision are outcomes of controlled behavior across multiple stages. They are not created at the end. They are preserved from the beginning.
In investment castings India, consistent output comes from keeping each variable within range so that none of them amplifies the other. When that happens, the casting does not need to be fixed. It simply comes out right, repeatedly.